Full-size furniture, printed in one piece.
Chairs, table bases, shelving and wall panels with up to 1.7 m of continuous print length. Recycled and wood-filled pellets, with pigments mixed into the feed for your own colors and effects.
- ▸Fewer joints, less hardware, less assembly
- ▸Recycled and wood-filled pellets
- ▸Validate your design and material with a paid sample print before you invest
Or start with your industry
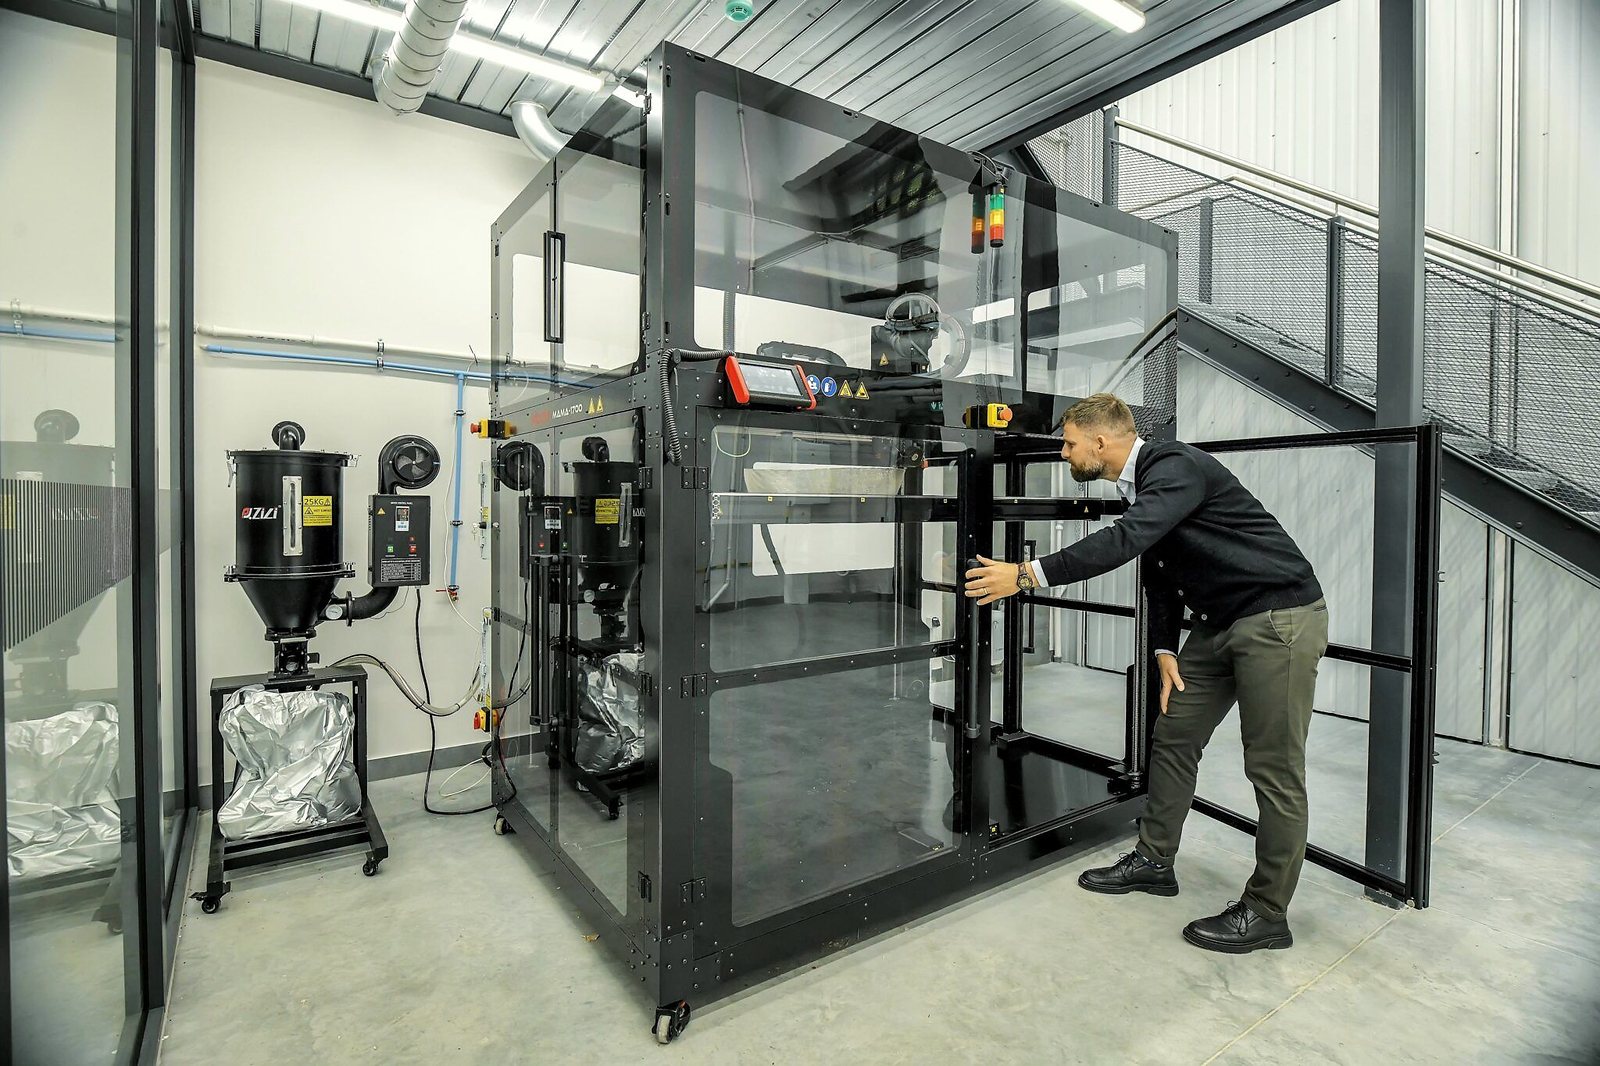
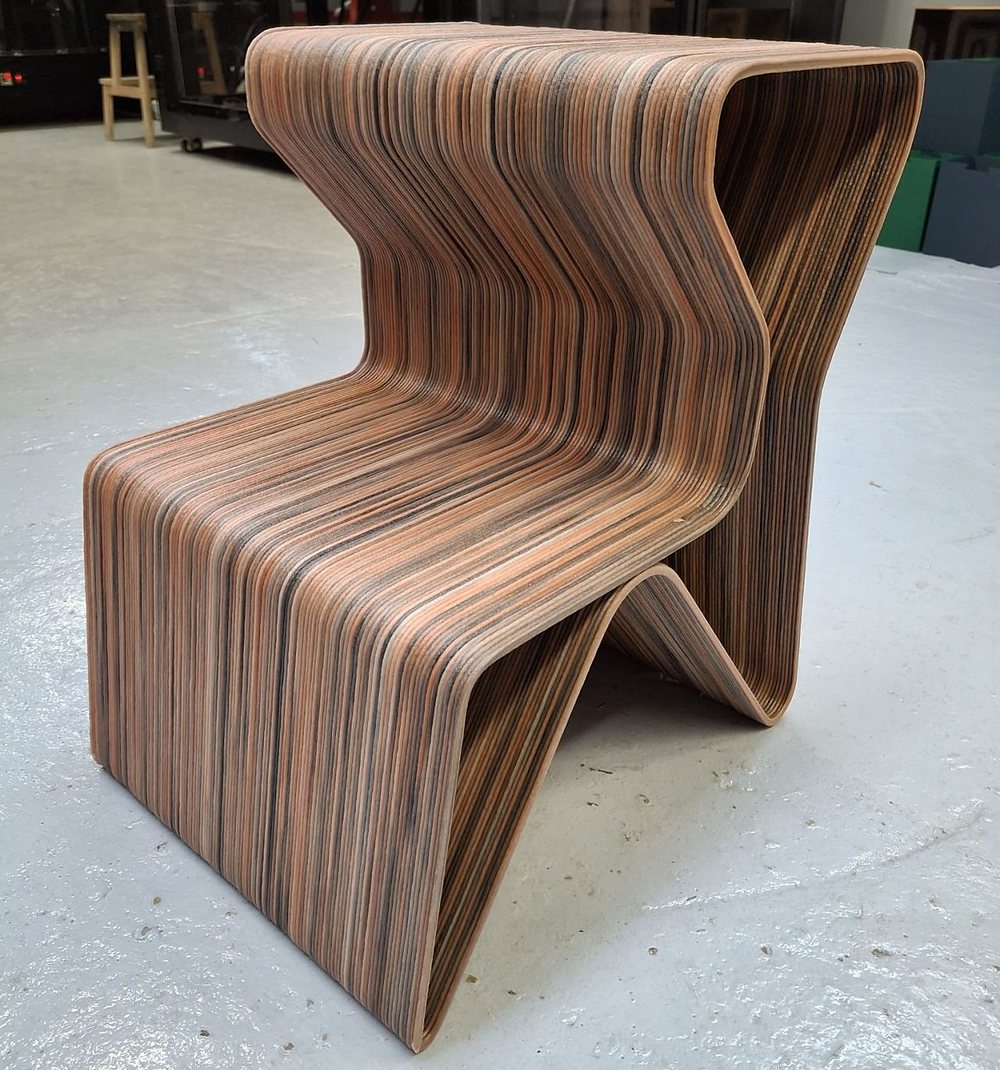 Furniture scaleChairs, tables, shelving, wall panels
The MAMA line
Three lengths. One pellet platform.
Every MAMA runs the pellet and the filament head on the same electronics and the same program. Pick the length your parts need, or let the application assessment pick it.
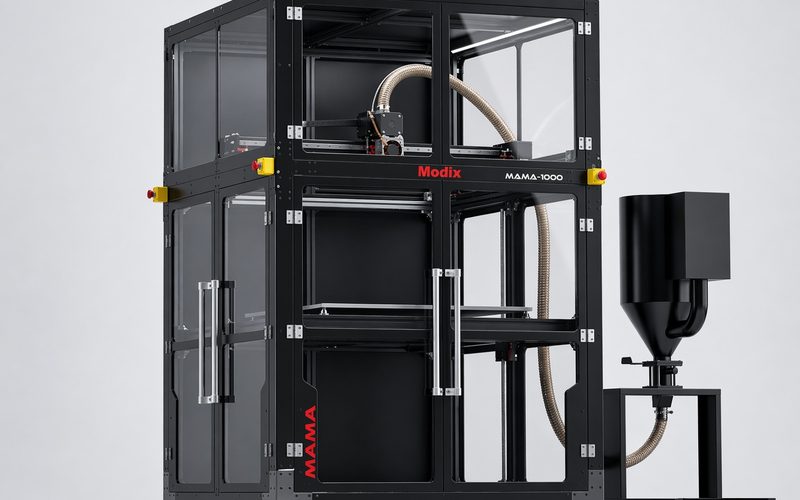 Studio and shop floor
MAMA-1000
1,000 × 1,000 × 1,000 mm39.4 × 39.4 × 39.4 in
- One cubic meter of build volume
- Pellet extrusion up to 3 kg/h
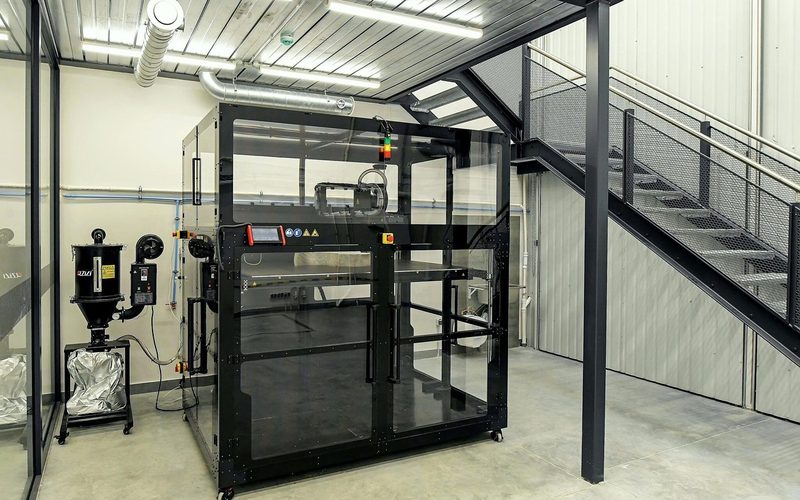 Furniture scaleYou are here
MAMA-1700
1,700 × 1,000 × 1,000 mm66.9 × 39.4 × 39.4 in
- 1.7 m continuous print length
- Lower feedstock cost than equivalent filament
 Automotive and aviation
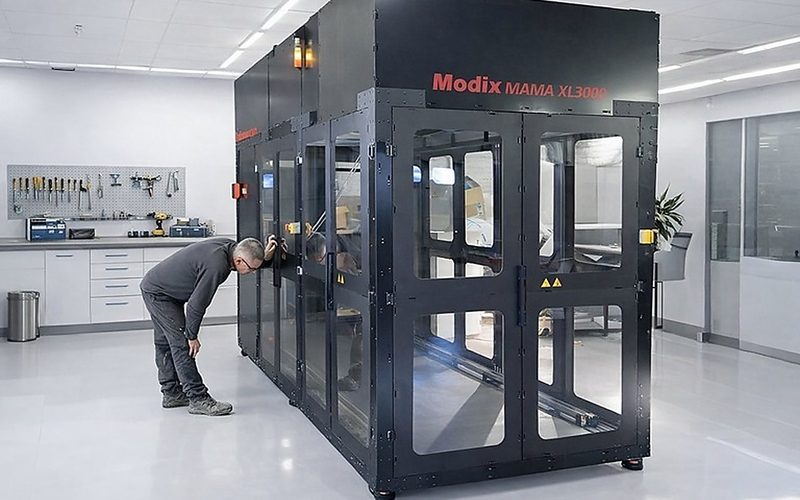
MAMA XL-3000
3,000 × 1,000 × 1,000 mm118.1 × 39.4 × 39.4 in
- 3 m continuous single-piece parts
- Full enclosure system included
Furniture
Built for furniture, printed in one piece.
Chairs, tables and shelving are where pellets pay off first: large, mostly hollow parts, recycled and wood-filled grades, and color mixed in at the feed instead of painted on.
Chairs and seating
Complete chairs and chair shells in one piece, with striped or solid color from masterbatch.
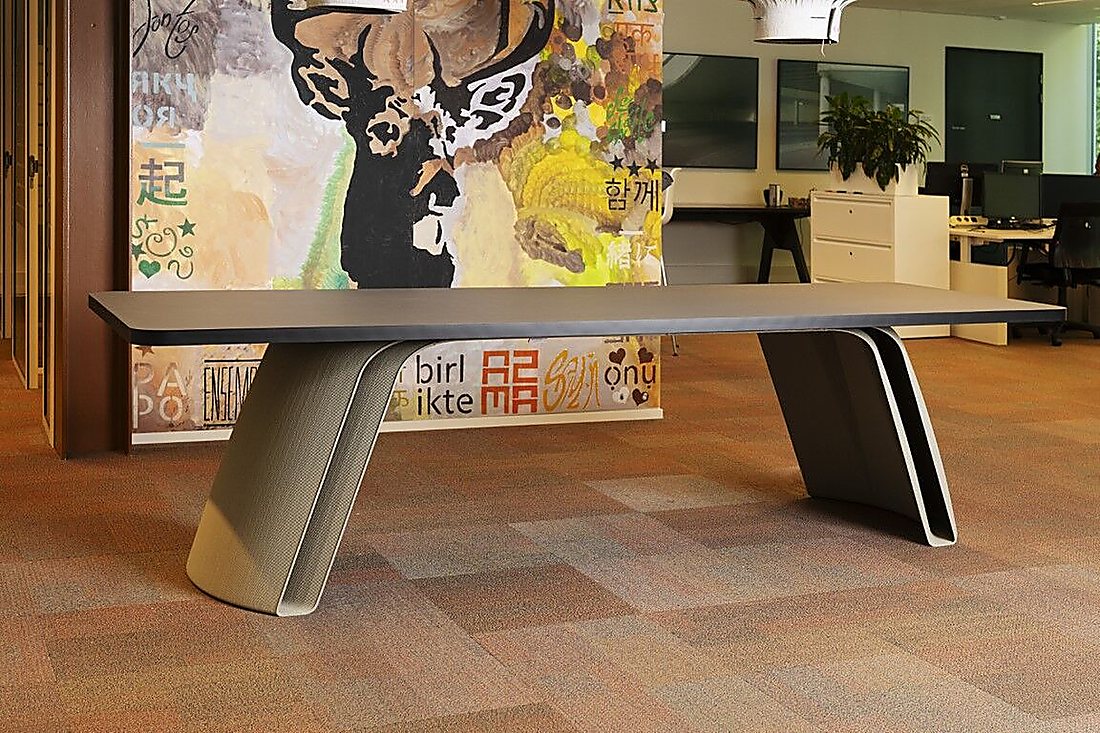
Table bases
Bases and legs as one part: fewer joints and no hardware to fit.
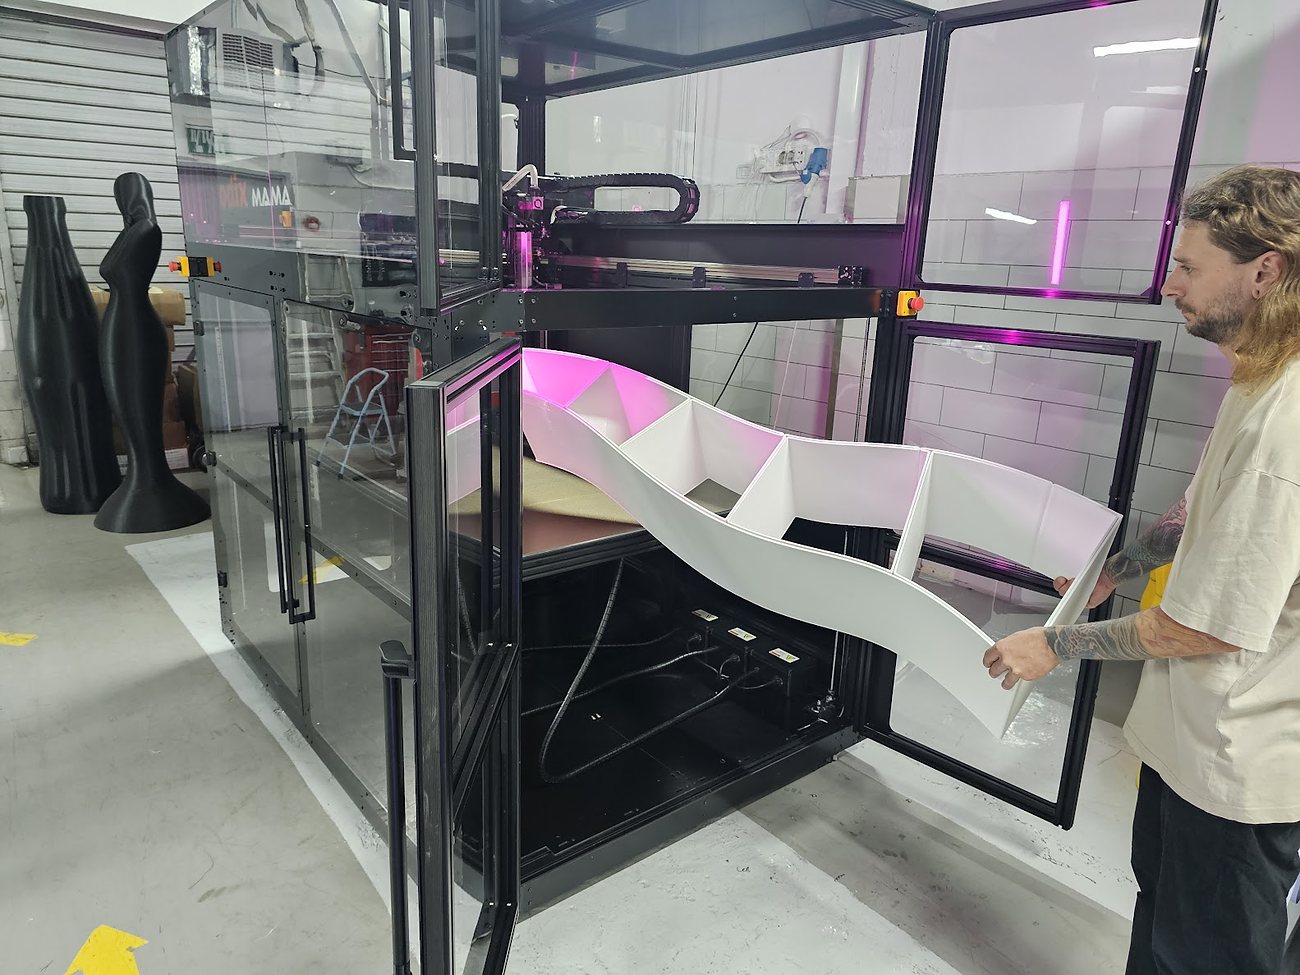
Shelving and storage
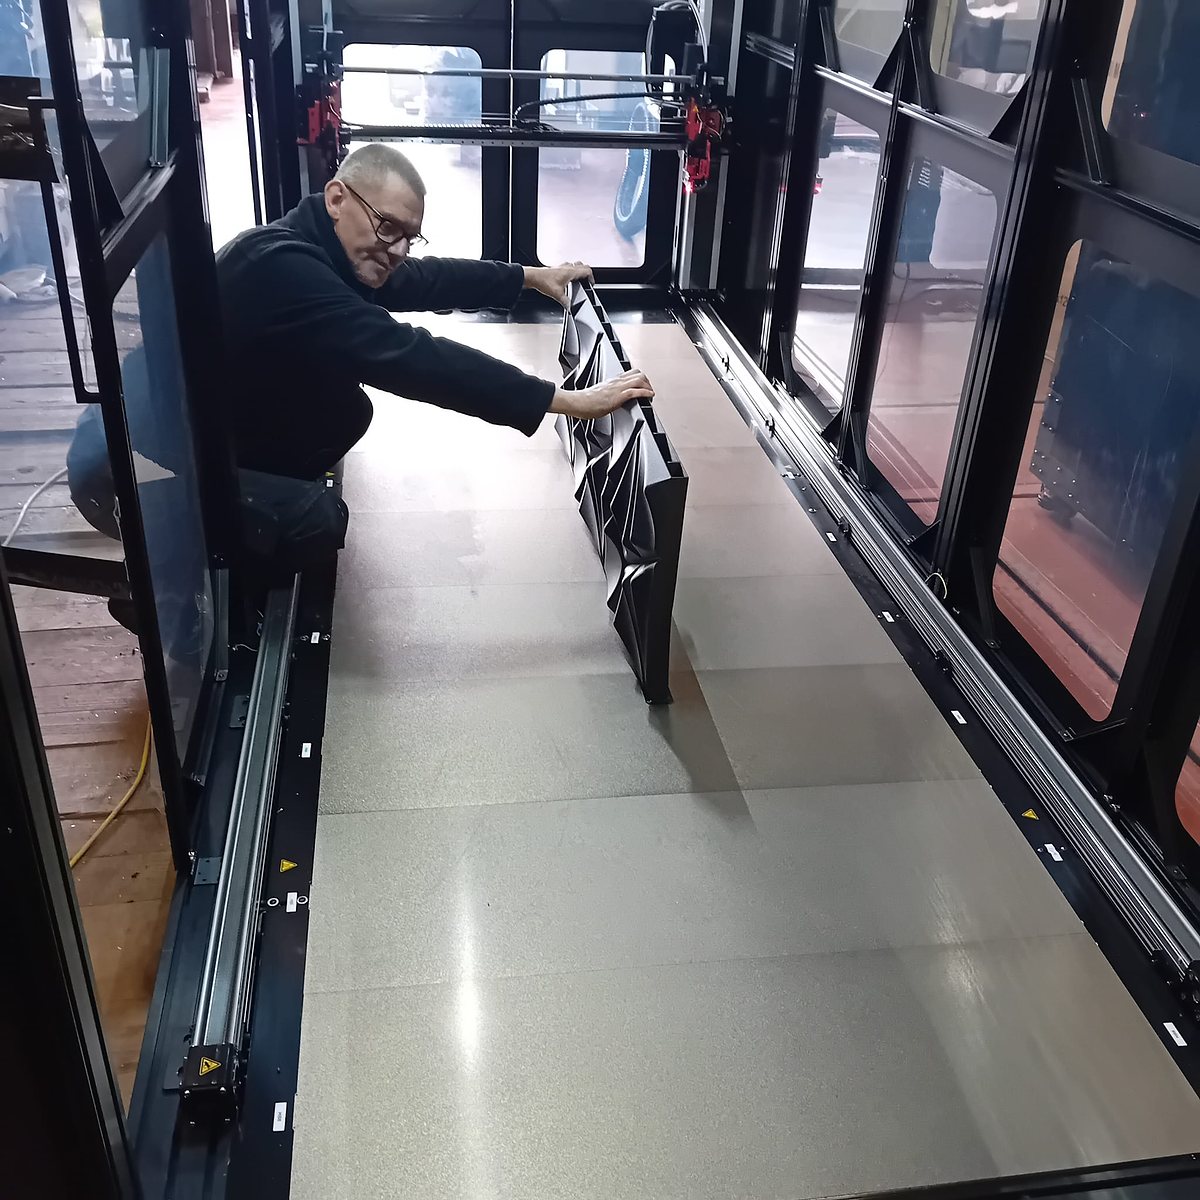
A 1.7 m bookshelf pulled off the bed in one piece.
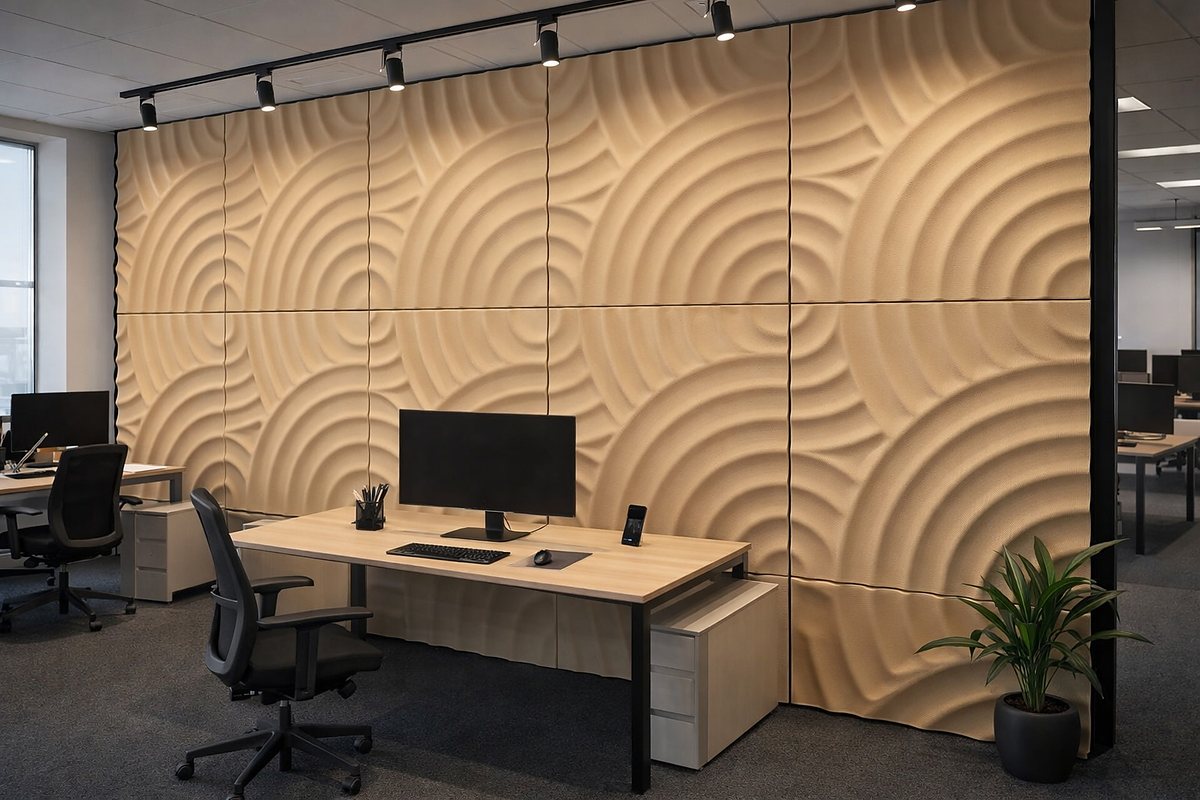
Wall panels and interiors
Panel systems with texture printed in, at architectural size.
1,700 × 1,000 × 1,000 mm covers a bench, a table base or a full-height shelf in one print.
What you buy
You get a solution to your needs.
We review your application, recommend a material and printer configuration, and quote a validation print. Once the application is approved, we build your MAMA-1700, commission it on site and train your operators.
Needs evaluation
We review your part, material, finish and production requirements, and tell you whether a MAMA is the right tool. If it is not, we say so.
Sample printing
Test a sample in the agreed material before you buy a printer. A paid service, quoted per part.
Built to order
We configure the machine and develop a print profile around your approved part.
On-site onboarding and training
We commission the printer on your floor and train your operators on your part.
Lifetime support
Technical support for the life of the printer, with application advice, spare parts and upgrades available.
Step one is yours: tell us about the part.
- ✓Reviewed by a pellet application engineer
- ✓A straight answer if a MAMA is not the right tool
- ✓A sample print before any machine decision
Print logs
Real parts. Real numbers.
Printed from pellets on MAMA machines. Weight, hours, nozzle and layer as logged, and which MAMA each part fits. If your part is not here, that is exactly what the application assessment is for.
FurnitureBookshelf, 1.7 m tall
Pulled off the bed in one piece, with nothing to assemble.Fits the MAMA-1700 in one piece. Printed on a MAMA-1700, lying flat along the 1.7 m axis.
- Height
- 1.7 m
- Material
- PLA pellets
- Parts
- 1
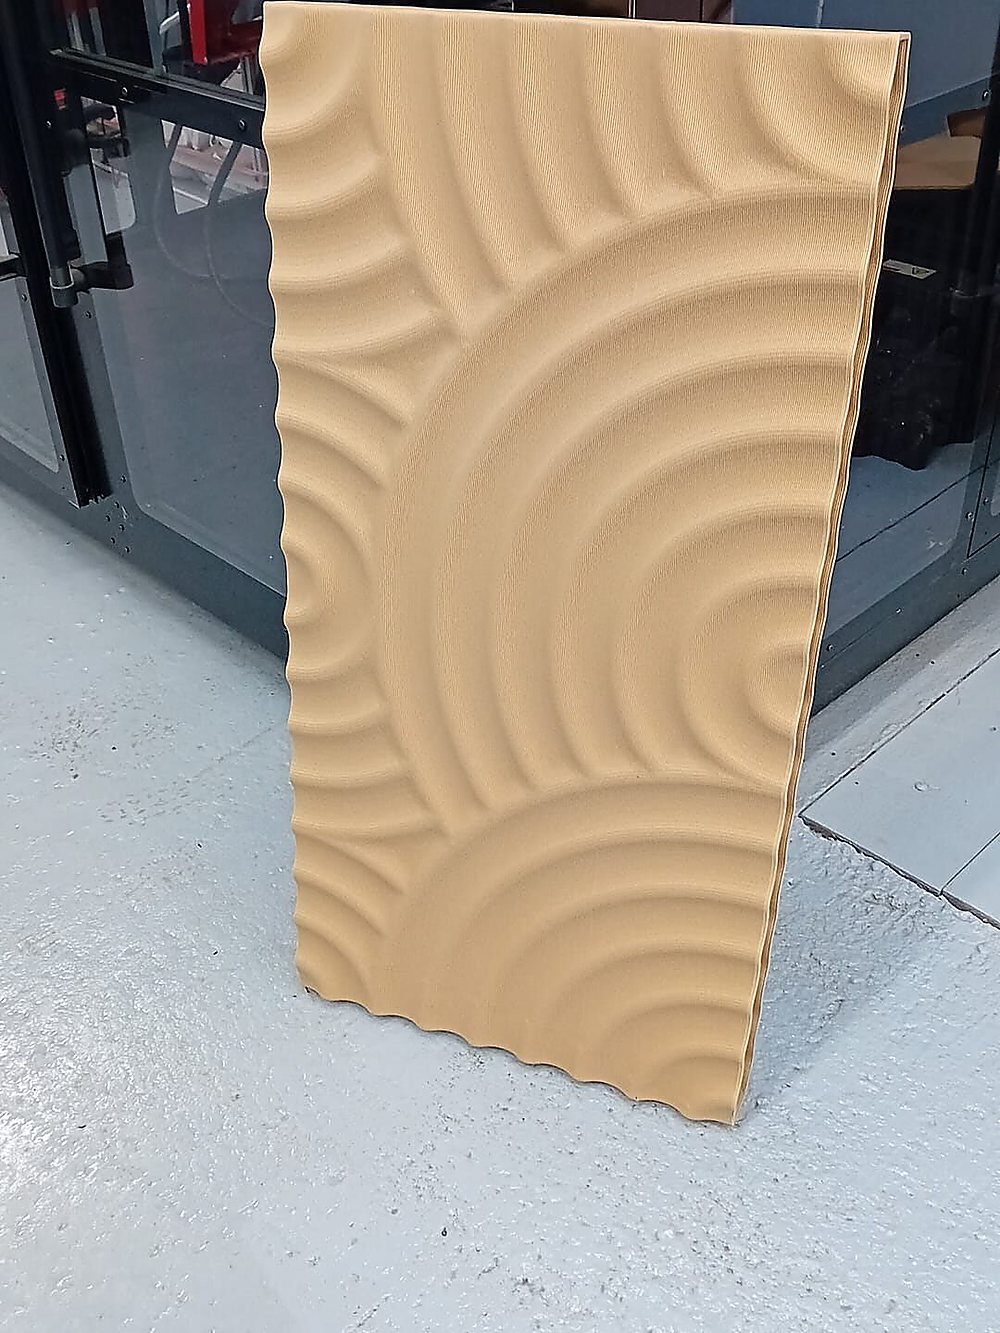 Interiors
Decorative panel
Masterbatch mixed in the feed gives color and matte effects with no painting.
- Weight
- 5.5 kg
- Print time
- 4.5 h
- Nozzle
- 5 mm
- Layer
- 3 mm
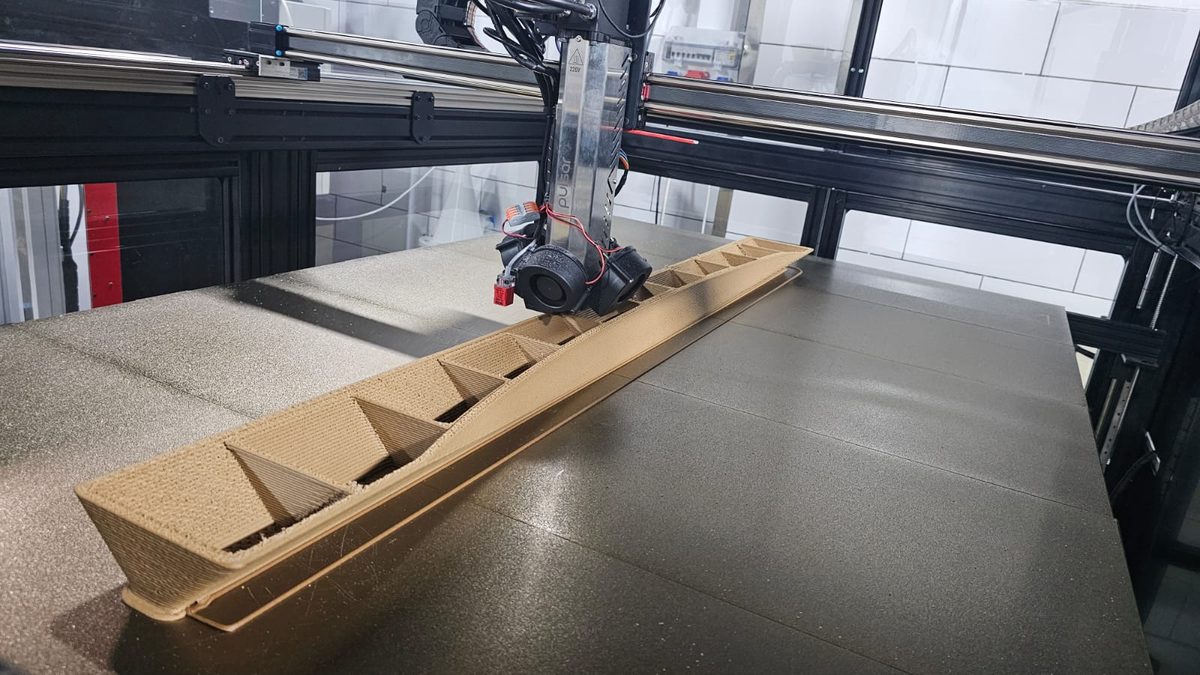 Tooling
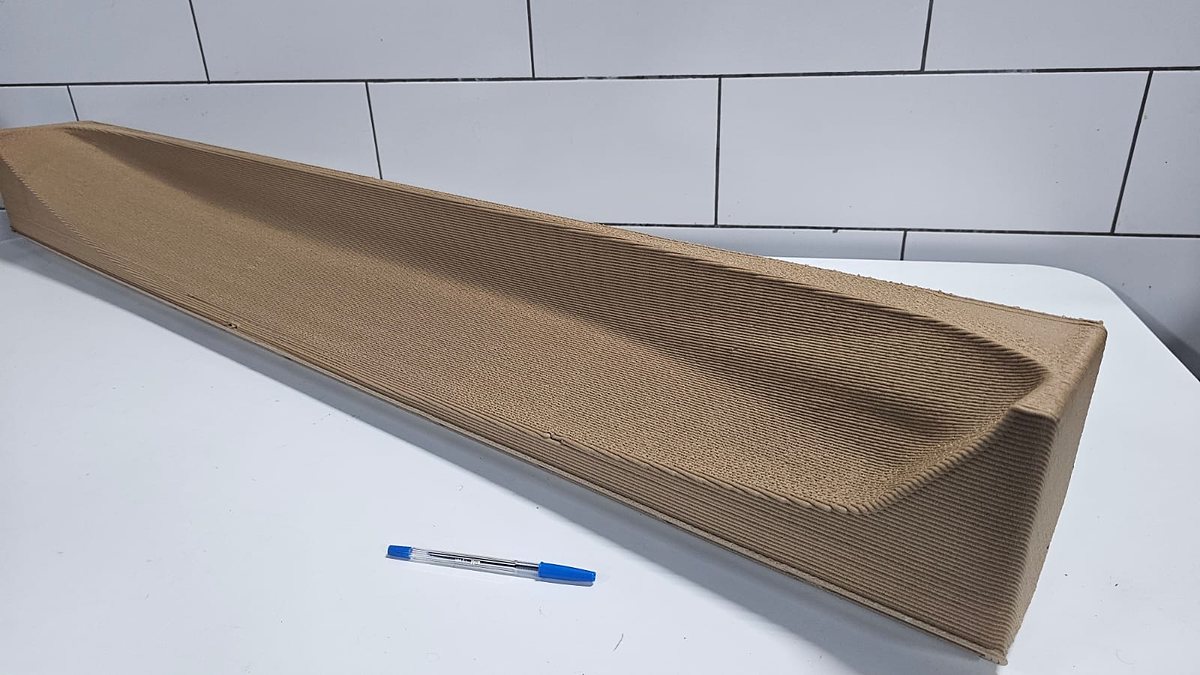
Low-temperature mold, 1.4 m
Wood-filled PLA pellets. The filler makes sanding, drilling and sealing straightforward.Fits the MAMA-1700 in one piece. 1,400 mm long, printed lying flat along the bed.
- Length
- 1.4 m
- Weight
- 7 kg
- Print time
- 5 h
- Nozzle
- 3 mm
- Layer
- 2 mm
- Material
- Wood PLA
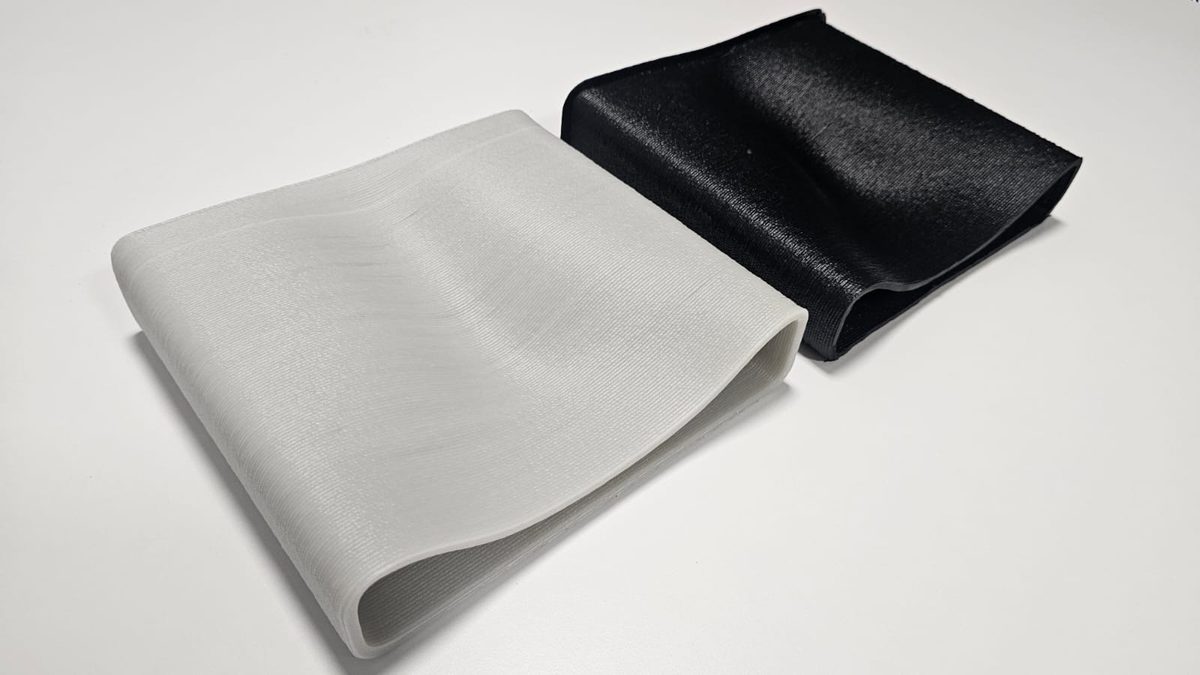
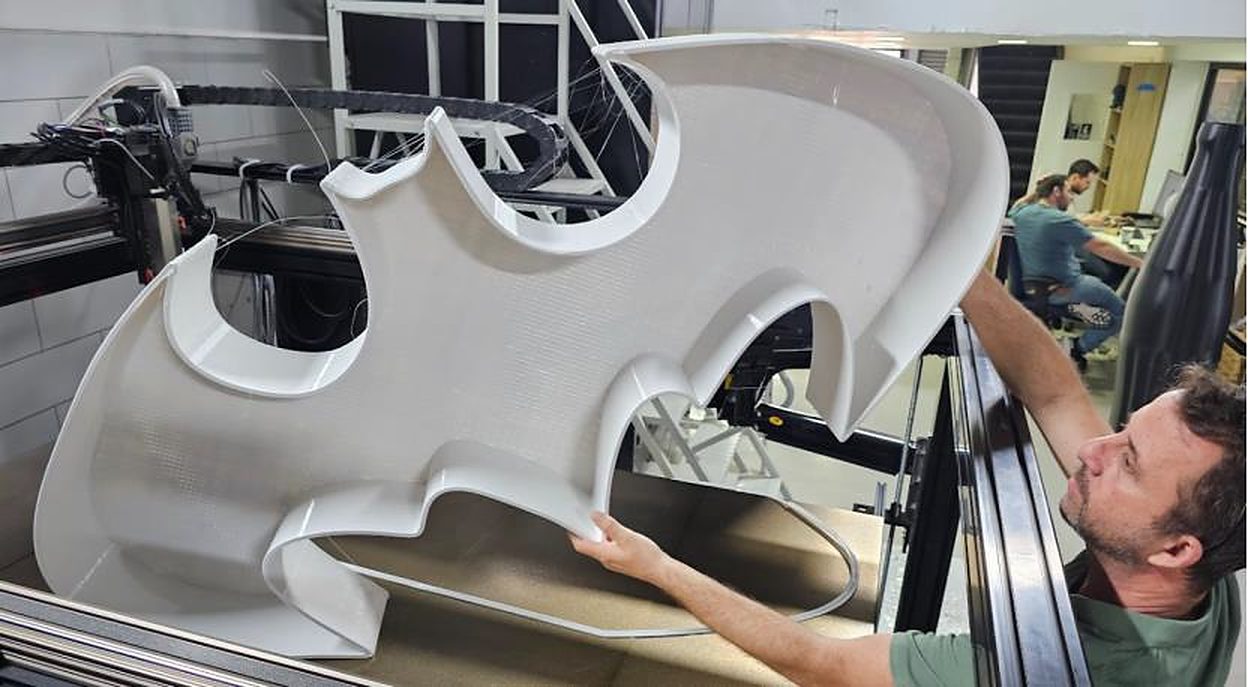 Signage
Large sign, one piece
Flame-retardant grades where public installation requires it.
- Weight
- 10.1 kg
- Print time
- 8.75 h
- Nozzle
- 5 mm
- Material
- PLA + masterbatch
 Composites
Carbon and glass-filled PETG
Fibers cut shrinkage and warping, and carbon sheds heat for shorter layer times.Fits the MAMA-1700 in one piece.
- Size
- 220 × 230 mm
- Print time
- ~1 h
- Height
- 50 mm
- Nozzle
- 3 mm
- Layer
- 1.5 mm
Application assessment
Tell us about your application. We put an engineer on it.
Tell us about your part, material and production goals. An application engineer reviews your answers and recommends the next step. Three quick steps, about two minutes.
- What you getAn initial material and process recommendation for your part
- ThenA discussion, and a sample-print quote where it fits
Which industry is the part for?
What is the part?In a few words
How big, roughly?A rough size is fine
Enter the length, width and height of your part.
How many?
What must the material do?Pick all that apply
Your assessment
Assessment received.
A pellet application engineer reviews it and comes back to you, usually within one business day.
New to pellets?
How pellet printing works.
Most MAMA customers have never printed from pellets. Here is the whole process, what changes compared with filament, and how to design for it. Onboarding covers every step on your own part.
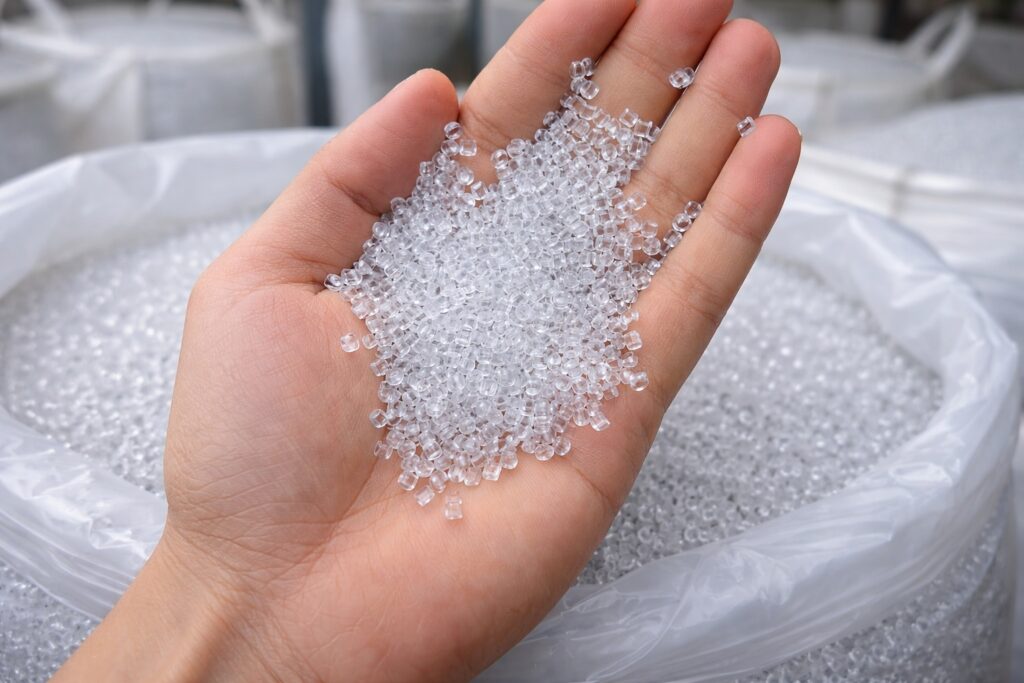 01Feedstock
Plastic pellets, 3 to 5 mm, the same feedstock injection molding uses. Virgin, recycled or filled.
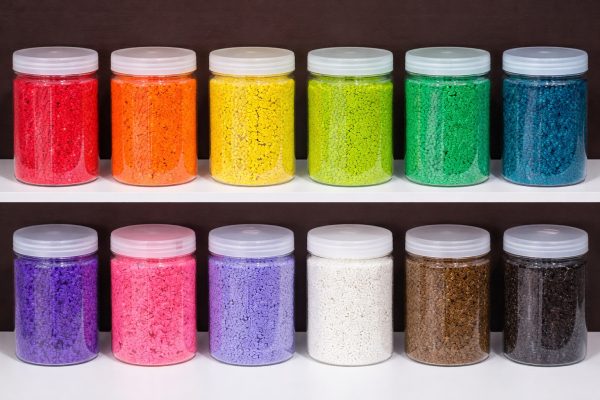 02Color
Masterbatch is mixed in by weight. About 5% white with 2 to 3% black gives a dark gray.
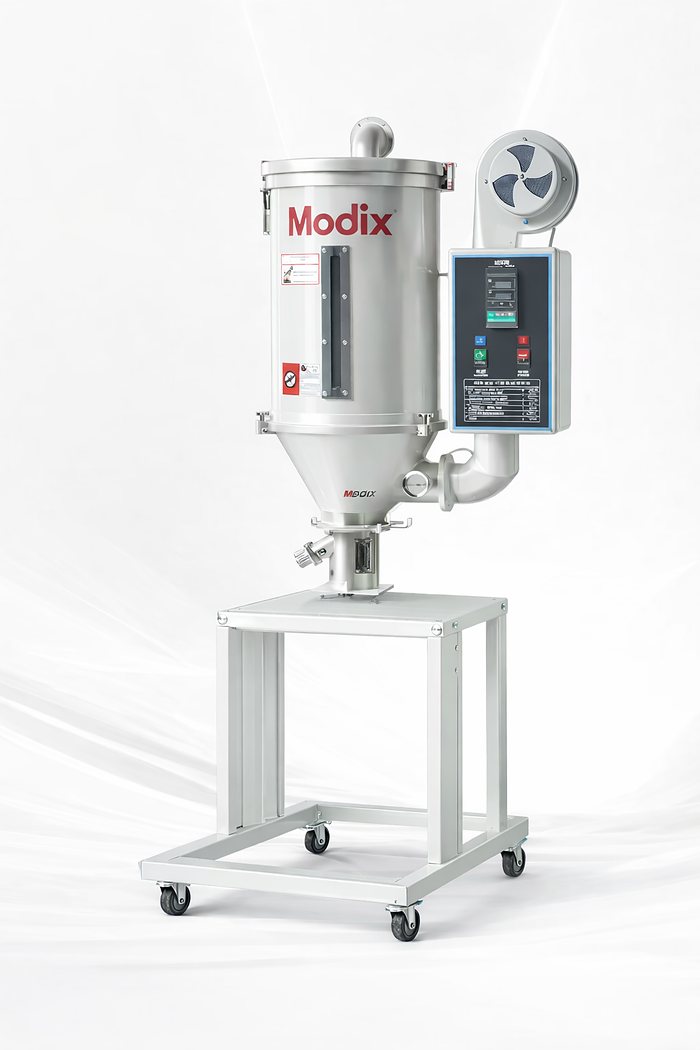 03Dry
PLA dries at 45 °C for 8 hours. PETG and nylon pick up moisture in minutes, so they dry every run.
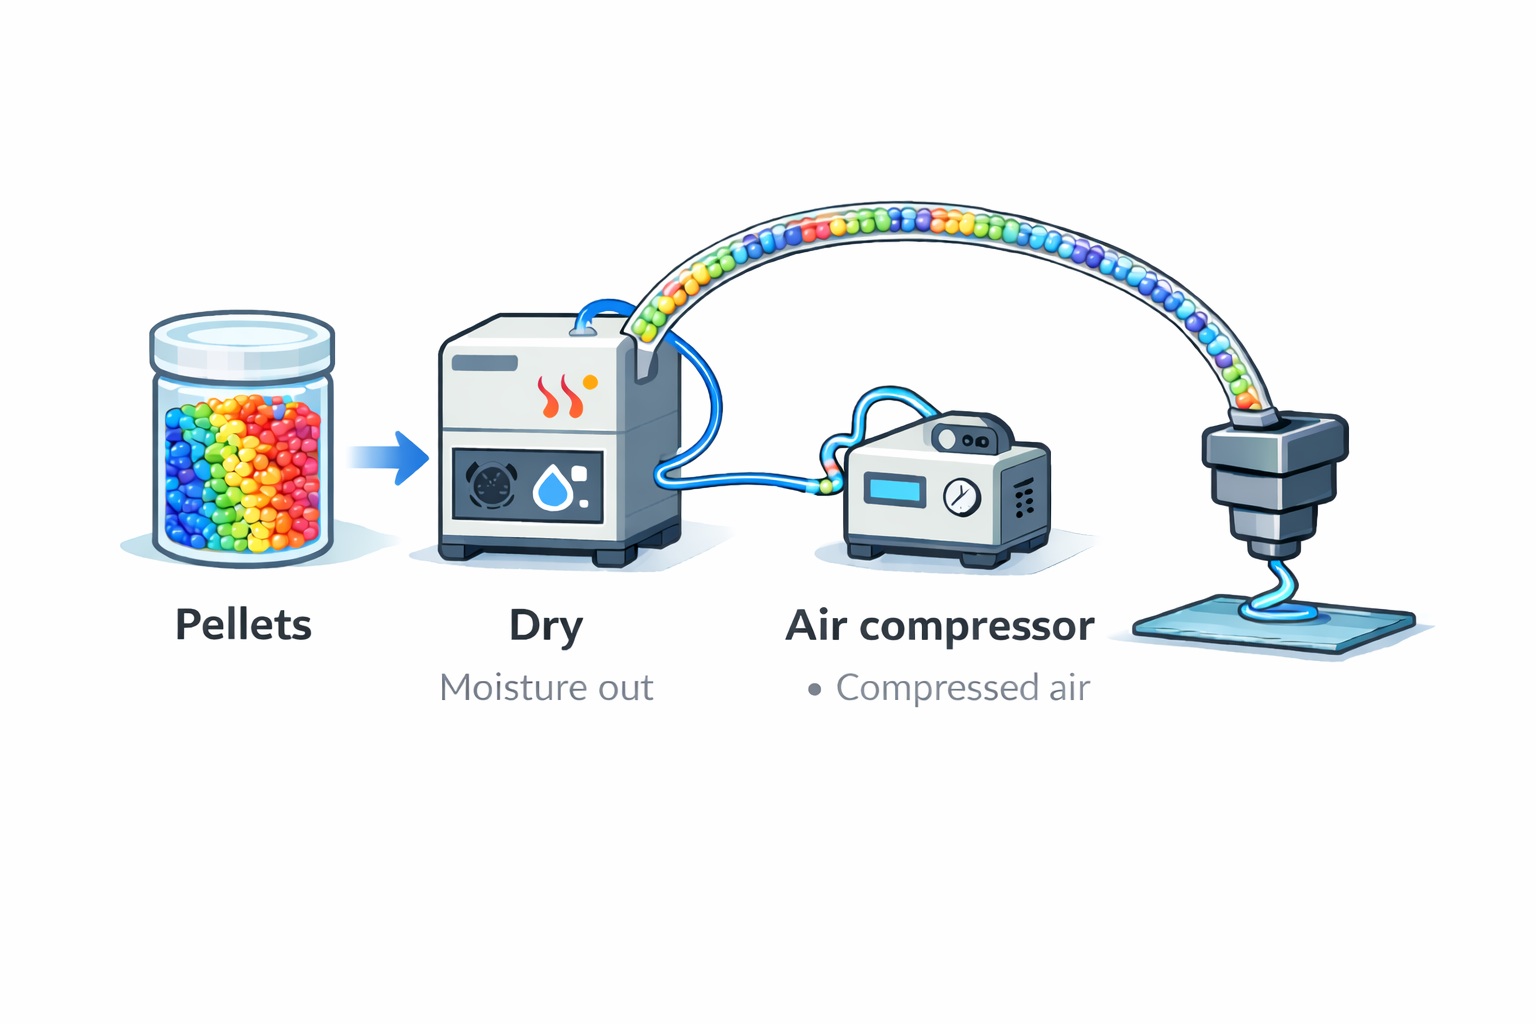 04Feed
Compressed air carries pellets from the hopper to the head. A level sensor keeps it topped up.
 05Melt and print
A screw with three heat zones melts the pellets, cooler at the top and hotter at the nozzle. Beads are 3 to 14 mm wide.
 06Finish
Sand, drill, seal and paint. Wood-filled grades finish like pattern-shop material.
Pellets versus filament
| Pellets (MAMA) | Filament | |
|---|---|---|
| Material cost | $2 to $8 per kg (typical, by grade and quantity) | $20 to $80 per kg |
| Output | Up to 3 kg/h | Up to 0.5 kg/h on the Griffin Ultra |
| Bead and layer | 3 to 14 mm wide, layers up to 3 mm | Finer: 1.6 mm nozzle, thinner layers |
| Material choice | Virgin, recycled, filled, your own compounds | What is sold as 1.75 mm filament |
| Supports | Not practical. Orientation solves it | Possible, soluble with Dual Filament (IDEX) |
| Preparation | Dry the pellets, fill the hopper | Load a spool |
| Surface | Visible layers. Sand and paint for show parts | Smoother as printed |
Designing for pellets: show the 8 rules
Thick pellet layers sag past 45° and pellet supports fuse to the part. Orient it, chamfer under ledges, or use Dual Filament (IDEX) for soluble supports.
On a large part the inside is where the hours go. Shell every solid; 10 to 25% infill gives most of the strength, above 50% is paying for nothing.
1 mm: up to 2.5 mm line, 0.75 mm layer. 3 mm: 8 mm line, 2 mm layer. 5 mm: 14 mm line, 3 mm layer. Walls in whole beads.
Round every corner (5 to 10 mm over 500 mm), break up flat floors, keep walls within a factor of 2, let the part cool on the bed.
Scale = 100 ÷ (100 − shrink %). A 1,000 mm part at 0.8% shrinks 8 mm. Calibrate at full size, X and Y apart from Z.
Half a bead in XY and half a layer in Z on faces you machine, solid pads under bores, critical faces vertical.
Spiral (vase) mode and single walls keep extruder pressure steady and cut print time.
Hours = part mass ÷ real throughput (1.15 to 1.4 kg/h on our logged prints), plus 10 to 30% for travel and slow layers.
The machine
Two print technologies, one platform.
Pellet for throughput, filament for detail. The MAMA-1700 takes either head on the same motion system, so the application decides and the decision is never permanent.
FGF pellet
Dyze Design Pulsar
Prints straight from plastic pellets, the same feedstock injection molding uses. No filament conversion, no filament markup.
FFF filament
Modix Griffin Ultra
Swaps in where the part needs finer features, tighter interfaces and a smoother surface. Same machine, same bed, same profile library.
| Material | Grade printed on the MAMA | Nozzle °C | Drying |
|---|---|---|---|
| PLA | NatureWorks Ingeo 2003D | 200 | 45 °C, 8 h |
| PLA | NatureWorks Ingeo 7003D | 180 to 190 | 45 °C, 8 h |
| Wood-look PLA | Mitsubishi Light Wood | 200 | 45 °C, 8 h |
| Cellulose-fiber composite | UPM Formi 3D 20/19 | 220 | 80 °C, 8 h |
| Recycled PETG | Mitsubishi rPETG | 220 | 70 °C, 8 h |
| Recycled PETG, 15% carbon fiber | Mitsubishi rPETG CF15 | 220 to 240 | 80 °C, 4 h |
| PETG, 20% glass fiber | Polyram PETG GF20 | 220 to 240 | 80 °C, 4 h |
| PETG, glass fiber | Polyful 2506 NC901 GF | 230 to 240 | 70 °C, 6 to 8 h |
25 kg batch. Moisture in the feedstock is the most common cause of a failed pellet print.
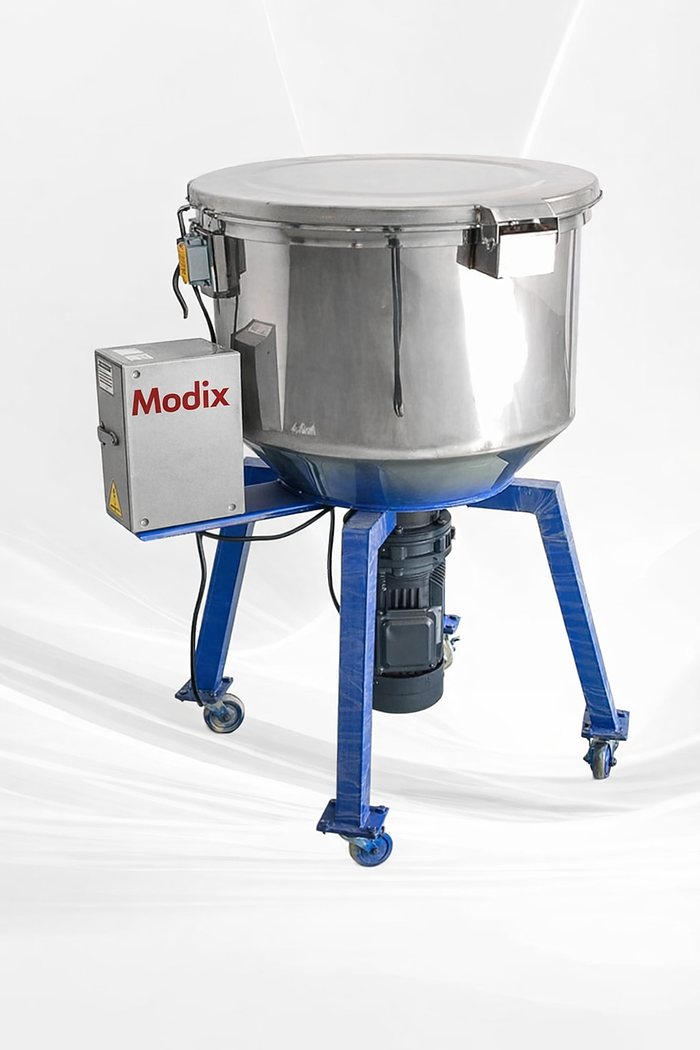
50 kg batch, 45 to 50 kg/h. Blend color and additives yourself, match a RAL or Pantone.
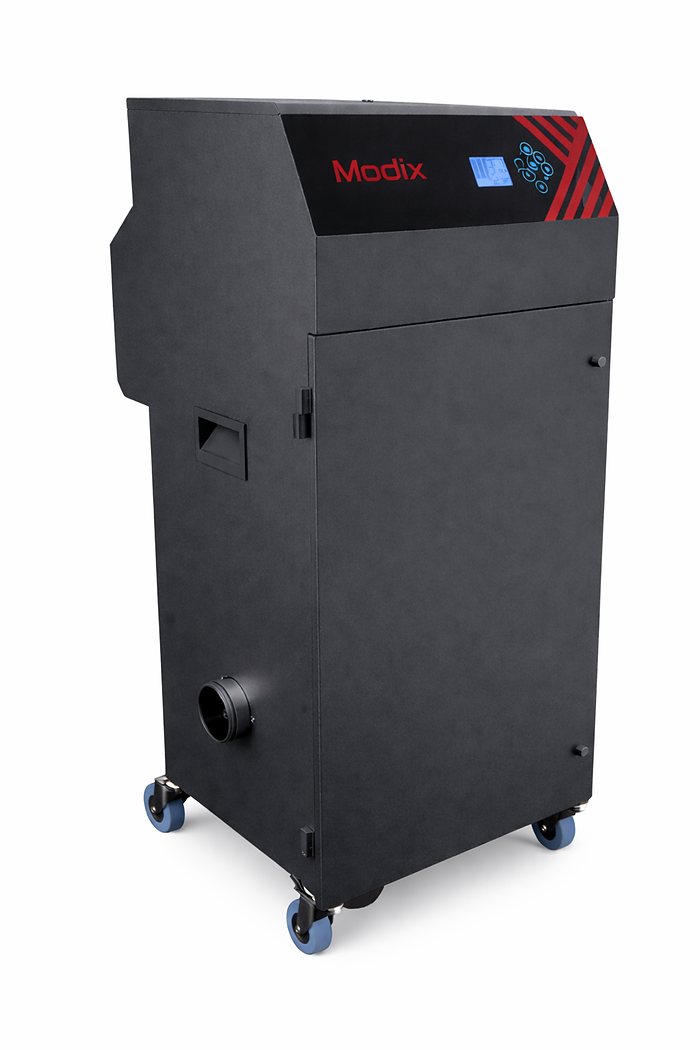
HEPA and activated carbon at 99.995%, 550 m³/hour, matched to the MAMA enclosure.
Door switches are part of the safety loop. Open a door in production and motion stops.
Production: doors locked, printing allowed. Maintenance: doors open, manual moves and calibration.
A hardware emergency stop loop, plus a status tower: green running, amber maintenance, red stop.
Pellet level, clog and cooling alarms pause the job and wait for the operator.
Throughput. Large parts, low material cost, composite and recycled feedstock.
Detail. Finer features, tighter tolerances, smoother surfaces.
Two independent Griffin Ultra heads, soluble supports, auto filament change.
MAMA-1700 specifications Compare all models →
FAQ
Pricing, samples and support.
Why is there no price on this page?
Is the sample print really paid?
Does the machine arrive assembled?
Can we maintain and upgrade it ourselves?
Pellet or filament, how do we choose?
Why an assessment and not a quick form?
We have never printed with pellets. Is that a problem?
Can it run recycled material or our own compounds?
What does it need on site?
What happens if the feed runs out mid-print?
Step one
Tell us about your application.
Three quick steps. A pellet application engineer reviews every answer, then we talk, and if the MAMA-1700 fits your part, we print it for you first.